
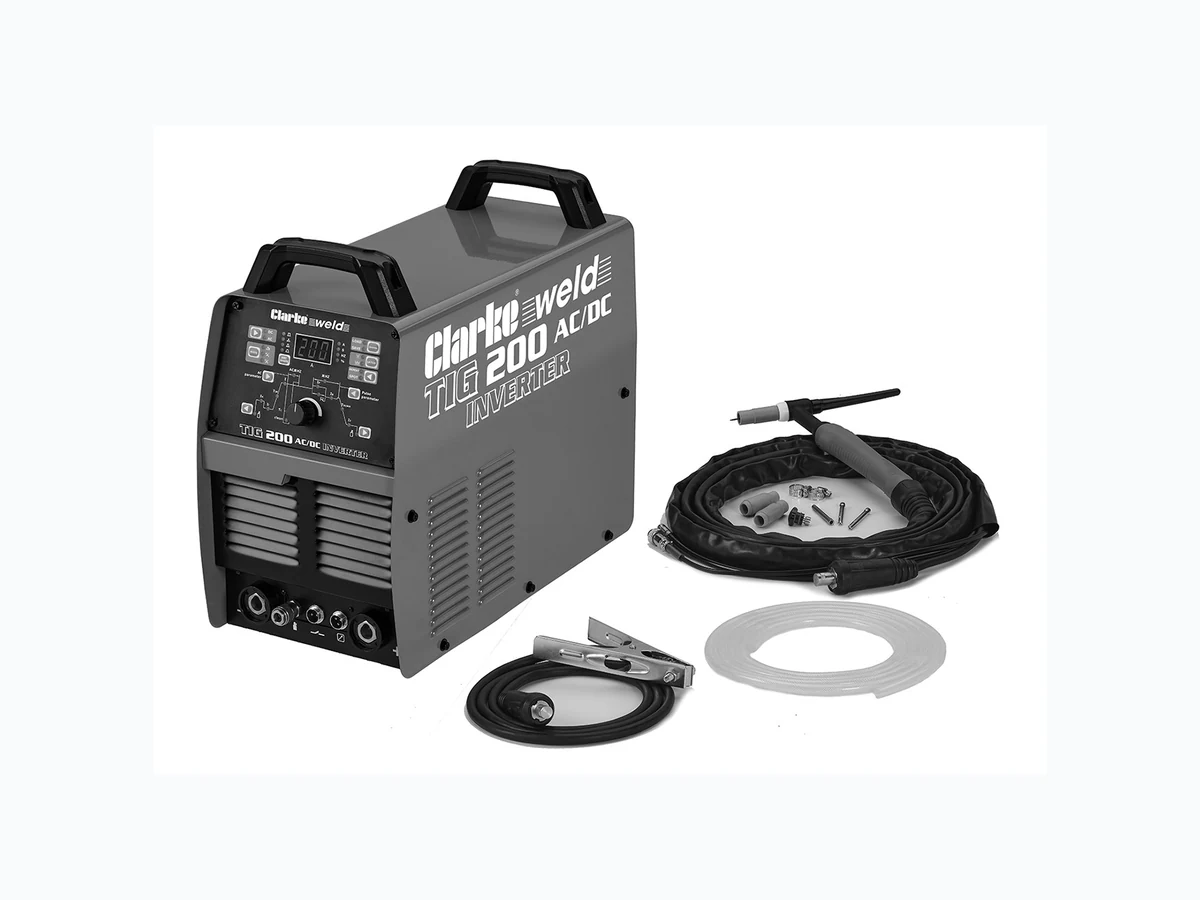
6012103 CLARKE
Document overview
- Manufacturer or author: Provided By digicamel.com
- PDF pages: 36
Technical content
OPERATION & MAINTENANCE INSTRUCTIONS ORIGINAL INSTRUCTIONS GC07/25 - rev 1 AC/DC TIG WELDER MODEL NO: TIG200 PART NO: 6012103
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com INTRODUCTION Thank you for purchasing this CLARKE Welder. Before attempting to operate the machine it is essential that you read this manual thoroughly and carefully follow all instructions given. In doing so you will ensure the safety of yourself and that of others around you, and you can also look forward to the welder giving you long and satisfactory service. When unpacking, any damage or deficiency should be reported to your CLARKE dealer immediately. A wide selection of accessories and consumables are available from your CLARKE dealer. SPECIFICATIONS NOTE: The details and specifications contained herein, are correct at the time of going to print. However, CLARKE International reserve the right to change specifications at any time without prior notice. TIG200 Unpacked Weight (kg) 15.85 Dimensions (L x W x H) (mm) 450 x 210 x 410 Power Supply 230V~ 50Hz Connecting plugs (32A) Peak Input Power 6.44 kw Peak Input Current 28A Max Output Welding Current TIG 200A/MMA 160A IP Rating IP21 Insulation Grade Class 1 - Grade H Suitable electrode size TIG 1.6, 2.0, 2.4 mm Welding Capacity 5mm (Mild Steel) 3mm (Aluminium
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com PRINCIPLES OF THE MACHINE The TIG200 Multi is an AC/DC inverter type welding machine which adopts advanced pulse width modulation (PWM) technology and insulated gate bipolar transistor (IGBT) to convert the power frequency to intermediate frequency, thereby replacing the bulky in the traditional arc welding machine with a small intermediate frequency transformer. The power frequency (low frequency) transformer gives the machine the advantages of small size, light weight, low noise, low power consumption and convenient portability. The welding machine is equipped with a digital panel, which has powerful functions and a wide range of parameter adjustment. TIG-200 can realize the following 5 welding methods through different combinations of the front panel selection switches:
- DC Manual Arc welding (DC MMA) ●DC Argon Arc welding (DC TIG)
- AC TIG welding (AC TIG) ●Pulse TIG welding (Pulse TIG)
- AC Pulse TIG (AC Pulse TIG) 1. DC Manual Arc Welding can choose different polarity connections according to different electrodes. 2. DC Argon Arc Welding generally adopts DC positive connection (workpiece connected to positive electrode, welding torch connected to negative electrode), which has the advantages of stable and concentrated arc, less damage to the tungsten electrode, relatively large welding current, and narrow and deep welds. 3. AC Argon Arc Welding can be achieved by adjusting the front panel cleaning effect knob to meet the needs of cleaning the oxide film, but also to obtain the largest penetration and the smallest tungsten loss. 4. Pulse Argon Arc Welding uses a base current to maintain the ionization channel of the main arc, and periodically adds a high peak pulse current of the same polarity to generate a pulse arc to melt the metal and control the droplet transfer. 5. AC Pulse Argon Arc Welding means that the pulse mode and the AC mode are mixed, and a more perfect welding process can be obtained.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com SUITABILITY OF DIFFERENT METHODS When using the welder in a gas-less configuration, the shielding gas is created from the flux within the welding wire rod. When using the welder outside you may need to erect a wind break to make sure the shielding gas is not blown away, thereby leaving a poor quality weld. ENVIRONMENTAL RECYCLING POLICY Through purchase of this product, the customer is taking on the obligation to deal with the WEEE in accordance with the WEEE regulations in relation to the treatment, recycling & recovery and environmentally sound disposal of the WEEE. In effect, this means that this product must not be disposed of with general household waste. It must be disposed of according to the laws governing Waste Electrical and Electronic Equipment (WEEE) at a recognised disposal facility. If disposing of this product or any damaged components, do not dispose of with general waste. This product contains valuable raw materials. Metal products should be taken to your local civic amenity site for recycling of metal products. MMA/Arc Welding Carbon Steel, Low Alloy Steel, Stainless Steel, Cast Iron. TIG Welding Carbon Steel, Low Alloy Steel, Stainless Steel, Cast Iron, Titanium, Copper + Brass. Metal Being Welded Suitable Gas Part number Mild Steel Carbon Dioxide (CO 2) 6000642 Stainless Steel Argon 6000663 Aluminium Thin Sheet Metal/Mild Steel Carbon Dioxide (CO2)/Argon Mix 6000662
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com SAFETY PRECAUTIONS FOR ALL WELDING FAILURE TO FOLLOW THESE RULES MAY RESULT IN SERIOUS PERSONAL INJURY. GENERAL PRECAUTIONS BURN PREVENTION Wear protective clothing - gauntlet gloves designed for use in welding, apron, and protective shoes. Button shirt collar and pocket flaps and wear cuffless trousers to avoid entry of sparks and slag. Wear helmet with safety goggles or glasses with side shields underneath, appropriate filter lenses or plates (protected by clear glass). This is a MUST for welding (and chipping) to protect the eyes from radiant energy and spatter. Replace cover glass when broken, pitted, or spattered. Avoid oily or greasy clothing. A spark may ignite them. Hot metal should NEVER be handled without gloves. First aid facilities and a qualified first aid person should be available, unless medical facilities are close by, for immediate treatment of flash burns of the eyes and skin. A hard hat should be worn when others work overhead. Flammable hair preparations should not be used by persons intending to weld or cut. NOTE: ALL protective wear incl. masks & head shields MUST comply with PPE Regulation (EU) 2016/425. TOXIC FUME PREVENTION Severe discomfort, illness or death can result from fumes, vapours, heat, or oxygen enrichment or depletion that welding (or cutting) may produce. Prevent them with adequate ventilation. NEVER ventilate with oxygen. Lead, cadmium, zinc, mercury and beryllium bearing materials, when welded (or cut) may produce harmful concentrations of toxic fumes. Adequate local exhaust ventilation must be used, or each person in the area as well as the operator must wear an air- supplied respirator. For beryllium, both must be used. Metals coated with or containing materials that emit toxic fumes should not be heated unless coating is removed from the work surface, the area is well ventilated, or the operator wears an air-supplied respirator. Work in a confined space only when it is being force ventilated and, if necessary, while wearing an air-supplied respirator. Vapours from chlorinated solvents can be decomposed by the heat of the arc (or flame) to form PHOSGENE, a highly toxic gas, and other lung and eye irritating by-products. The ultraviolet (radiant) energy of the arc can also decompose trichloroethylene and perchloroethylene vapours to form phosgene. DO NOT WELD where solvent vapours can be drawn into the welding WARNING: AS WITH ALL MACHINERY, THERE ARE CERTAIN HAZARDS INVOLVED WITH THEIR OPERATION AND USE. EXERCISING RESPECT AND CAUTION WILL CONSIDERABLY LESSEN THE RISK OF PERSONAL INJURY. HOWEVER, IF NORMAL SAFETY PRECAUTIONS ARE OVERLOOKED, OR IGNORED, PERSONAL INJURY TO THE OPERATOR MAY RESULT.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com atmosphere or where the radiant energy can penetrate to atmospheres containing even minute amounts of trichloroethylene or perchloroethylene. FIRE AND EXPLOSION PREVENTION Causes of fire and explosion are: 1. Combustibles reached by the arc, flying sparks, hot slag or heated material; 2. Short circuits. BE AWARE that flying sparks or falling slag can pass through cracks, along pipes, through windows or doors, and through wall or floor openings, out of sight of the goggled operator. To prevent fires and explosion: keep equipment clean and operable, free of oil, grease, and (in electrical parts) of metallic particles that can cause short circuits. If combustibles are in the area, DO NOT weld. Move the work if practicable, to an area free of combustibles. Avoid working in paint spray rooms, dip tanks, storage areas, ventilators. If the work cannot be moved, move combustibles away from sparks and heat; or protect against ignition with suitable fire-resistant covers or shields. Walls, ceilings, and floor near work should be protected by heat resistant covers or shields. Fire watcher must be standing by with suitable fire extinguishing equipment during and for some time after welding or cutting if: 1. Appreciable combustibles (including building construction) are within 10m. 2. Appreciable combustibles are further than 10m, but can be ignited by sparks. 3. Openings (concealed or visible) in floors or walls can expose combustibles to sparks. 4. Combustibles adjacent to walls, ceilings, roofs or metal partitions can be ignited by radiant or conducted heat. After work, check that area is free of sparks, glowing embers and flames. An empty container that held combustibles or that can produce flammable or toxic vapours when heated, must never be welded on or cut, unless the container has first been cleaned. This includes a thorough steam or caustic cleaning (or a solvent or water washing, depending on the combustible’s solubility) followed by purging and inerting with nitrogen or carbon dioxide, and using protective equipment. Water filling just below the working level may substitute for inerting. A container with unknown contents should be cleaned (see paragraph above). DO NOT depend on sense of smell or sight to determine if it is safe to weld or cut. Hollow castings or containers must be vented before welding as they can explode. In explosive atmospheres, NEVER weld or cut where the air may contain flammable dust, gas, or liquid vapours.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com DO NOT overload arc welding equipment. It may overheat cables and cause a fire. Loose cable connections may overheat or flash and cause a fire. NEVER strike an arc on a cylinder or other pressure vessel. It creates a brittle area that can cause a violent rupture or lead to such a rupture later under rough handling. ELECTRIC ARC WELDING Comply with precautions in above and this section. Arc welding, properly done, is a safe process but a careless operator invites trouble. The equipment carries high currents at significant voltages. The arc is very bright and hot. Sparks fly, fumes rise, ultraviolet and infrared energy radiates and work pieces are hot. The wise operator avoids unnecessary risks and protects himself and others from accidents. BURN PROTECTION The welding arc is intense and visibly bright. It’s radiation can damage eyes, penetrate lightweight clothing, reflect from light coloured surfaces and burn the skin and eyes. Skin burns resemble acute sunburn, those from gas - shielded arcs are more severe and painful. PROTECTIVE CLOTHING (PPE) MUST BE WORN Wear long sleeved clothing (particularly for gas shielded arc) in addition to gloves, apron and strong shoes. As necessary, use additional protective clothing such as leather jacket or sleeves, flameproof apron, and fire-resistant leggings. Avoid outer garments of untreated cotton. Bare skin protection: Wear dark substantial clothing, button collars closed to protect the chest and neck and button any pockets to prevent entry of sparks. EYE AND HEAD PROTECTION Protect eyes from exposure to arc. NEVER look at an electric arc without protection. Welding helmet or shield containing an appropriate filter plate (Please refer to the section ‘Welding Shield on page 16). Place over face before striking arc. Protect filter plate with a clear cover plate. Cracked or broken helmet or shield should NOT be worn; radiation can pass through to cause burns. Cracked, broken, or loose filter plates must be replaced IMMEDIATELY. Replace clear cover plate when broken, pitted, or spattered. WE SUGGEST you wear flash goggles with side shields under the helmet, to give some protection to the eyes should the helmet not be lowered over the face before an arc is struck. Looking at an arc momentarily with unprotected eyes (particularly high intensity gas-shielded arc) can cause a retinal burn that may leave a permanent dark area in the field of vision. Before welding whilst wearing contact lenses, seek advice from your optician. PROTECTION OF NEARBY PERSONNEL For production welding, a separate, well vented room or enclosed bay is best. In open areas, surround the operation with low reflective, non- combustible screens or panels. Allow for free air circulation, particularly at floor level. Provide face shields for all
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com persons who will be looking directly at the weld. Others working in the area should wear flash goggles. Before starting to weld, make sure that screen or bay doors are closed. SHOCK PREVENTION Exposed live conductors or other bare metal in the welding circuit, or in unearthed, electrically-LIVE equipment can fatally shock a person whose body becomes a conductor. DO NOT stand, sit, lie, lean on or touch a wet surface when welding without suitable protection. PROTECTION FOR WEARERS OF ELECTRONIC LIFE SUPPORT DEVICES (PACEMAKERS) Magnetic fields from high currents can affect pacemaker operation. Persons wearing pacemakers should consult with their doctor before going near arc welding or spot welding operations. PROTECTION AGAINST SHOCK Keep your body and clothing dry. NEVER work in damp area without adequate insulation against electric shock. Stay on a dry duckboard or rubber mat when dampness or sweat can not be avoided. Sweat, sea water, or moisture between body and an electrically LIVE part - or earthed metal - reduces the body surface electrical resistance, enabling dangerous and possibly lethal currents to flow through the body. EARTHING THE EQUIPMENT When arc welding equipment is earthed according to the National Electrical Code and the workpiece is earthed, a voltage may exist between the electrode and any conducting object. Examples of conducting objects include, but are not limited to, buildings, electrical tools, work benches, welding power source cases, workpieces, etc. NEVER touch the electrode and any metal object unless the welding power source is off. When installing, connect the frames of each unit such as welding power source, control, work table, and water circulator to the building earth. Conductors must be adequate to carry earth currents safely. Equipment made electrically live by stray current may shock, possibly fatally. DO NOT EARTH to electrical conduit or to a pipe carrying ANY gas or a flammable liquid such as oil or fuel. CABLES Frequently inspect cables for wear, cracks and damage. IMMEDIATELY REPLACE those with excessively worn or damaged insulation to avoid possibly lethal shock from bared cable. Cables with damaged areas may be taped to give resistance equivalent to original cable. Keep cable dry, free of oil and grease and protected from hot metal and sparks. TERMINALS AND OTHER EXPOSED PARTS Terminals and other exposed parts of electrical units should have insulating covers secured before operation.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com SAFETY DEVICES Safety devices such as interlocks and circuit breakers should not be disconnected or shunted out. Before installation, inspection, or service of equipment, shut off all power and remove line fuses (or lock or red-tag switches) to prevent accidental turning ON of power. DO NOT open power circuit or change polarity while welding. If, in an emergency, it must be disconnected, guard against shock burns, or flash from switch arcing. Always shut OFF and disconnect all power to equipment. A power disconnect switch must be available near the welding power source. GENERAL PRECAUTIONS FOR WELDING 1. ALWAYS ensure that there is full free air circulating around the outer casing of the machine and that the louvres are unobstructed. 2. A welding arc can seriously damage your eyes. Both operator and spectators must ALWAYS use a proper welding face shield or helmet with suitable filter lenses. Proper gloves and working clothes should be worn at all times. 3. ALWAYS remove all flammable materials from the welding area. 4. NEVER remove any of the panels unless the machine is disconnected from the supply and NEVER use the machine with any of the panels removed. 5. NEVER use or store in a damp environment. DO NOT expose to rain. 6. NEVER attempt any electrical or mechanical repair unless your are a qualified technician. If you have a problem with the machine contact your local CLARKE dealer. 7. ALWAYS keep a fire extinguisher handy (Dry Powder, C02 or BCF, NOT Water). 8. NEVER continue to weld, if, at any time, you feel even the smallest electric shock. Stop welding IMMEDIATELY and DO NOT attempt to use the machine until the fault is diagnosed and corrected. 9. NEVER allow the earth cable or torch to become wrapped around the operator or any person in the vicinity. A comprehensive range of CLARKE safety equipment for use when welding is available from your local dealer. See page 32. Consideration should be given to shielding the supply cable of permanently installed welding equipment, in metallic conduit or equivalent. Shielding should be electrically continuous throughout its length. The shielding should be connected to the welding power source so that good electrical contact is maintained between the conduit and the welding power source enclosure.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com The welding equipment should be routinely maintained according to the manufacturer’s recommendations (see page 28). Any access and service doors and covers should be closed and properly fastened when the welding equipment is in operation. The welding equipment should not be modified in any way except for those changes and adjustments covered in the manufacturer’s instructions. In particular, the spark gaps of arc striking and stabilizing devices should be adjusted and maintained according to the manufacturers recommendations. PREPARATION OF THE WORKING AREA The working area must be sufficiently spacious, not humid, and well-ventilated as to avoid any fumes which develop from the welding process and from incidental material adhering to the pieces to be welded (oils, paints, tars...) which may cause danger to the operator. Avoid welding tanks which may contain flammable residuals. WARNING: ELECTRIC SHOCK CAN BE FATAL. A PERSON QUALIFIED IN FIRST AID SHOULD ALWAYS BE PRESENT IN THE WORKING AREA. IF PERSON IS UNCONSCIOUS AND ELECTRIC SHOCK IS SUSPECTED, DO NOT TOUCH THE PERSON IF HE OR SHE IS IN CONTACT WITH THE WELDER OR CABLES. DISCONNECT THE WELDER FROM THE POWER SOURCE AND THEN USE FIRST AID. DRY WOOD OR OTHER INSULATING MATERIAL CAN BE USED TO MOVE CABLES, IF NECESSARY, AWAY FROM THE PERSON.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com SAFETY SYMBOLS The following symbols may be displayed on the machine or its packaging. Read this instruction booklet carefully before use. Do not expose to rain. Wear welding mask Recycle unwanted materials under WEEE Directive Wear protective gloves General Hazard Danger:- Arc Rays Wear a dust mask Caution:- Hot surface Warning;- Magnetic field created Risk of Electric Shock Danger! Harmful fumes May interfere with pacemakers Do not weld near flammable or combustible materials
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com ELECTRICAL CONNECTION This welder MUST be connected to a 230 Volt, 1 phase 50Hz supply through a suitably rated isolator switch. Before switching on, make sure that the voltage of your electricity supply is correct. Connecting it to another power source may cause damage. A suitable plug is available from your CLARKE dealer. The user may also purchase a suitable connecting cable capable of handling 32 Amps with a supply plug rated at 32A or better. A length of 2-3 metres is recommended giving mobility to the appliance but without becoming a trip hazard. Any such plug should be fitted following the wiring instructions shown below. If the colours of the wires in the power cable of this product do not correspond with the markings on the terminals of your plug, proceed as follows.
- The Blue wire must be connected to the terminal which is marked N or Neutral.
- The Brown wire must be connected to the terminal which is marked L or Live.
- The Yellow wire must be connected to the terminal which is marked E or Earth. If in any doubt, consult a qualified electrician. DO NOT attempt any repairs yourself. WARNING! READ THESE ELECTRICAL SAFETY INSTRUCTIONS THOROUGHLY BEFORE CONNECTING THE PRODUCT TO A POWER SUPPLY. THE INSTALLATION OF THIS APPLIANCE SHOULD BE CARRIED OUT BY A COMPETENT ELECTRICIAN AND BE IN ACCORDANCE WITH CURRENT IEE WIRING REGULATIONS (BS4343). WARNING: THE WIRES IN THE POWER CABLE OF THIS PRODUCT ARE COLOURED IN ACCORDANCE WITH THE FOLLOWING CODE: BLUE = NEUTRAL BROWN = LIVE YELLOW = EARTH Plug must be BS60309 approved.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com MACHINE OVERVIEW The TIG200 Multi- welder has the following features:
1 Quick connector (positive) 11 Welding waveform selection
2 Remote control socket 12 Channel and save selection button
3 Welding torch switch socket 13 2T/4T selection button
4 Solenoid valve output 14 Repeat/spot weld selection button
5 Quick connector (negative) 15 Pulse parameter selection button
6 Parameter adjustment knob 16 Weld parameter selection button
7 Welding selection button 17 Solenoid valve input connector
8 AC parameter selection button 18 Power cable entry connection
9 Welding mode selection button 19 Power switch
10 AC/DC selection button
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com THE MACHINE FEATURES AND CONTROL FUNCTIONS 1. Positive Quick connector
- Positive quick connector socket, for connection of grounding clamp. 2. Remote control cable socket
- Quick connecting remote control terminal. 3. Welding gun switch socket
- Quick connecting control switch cable of the welding gun. 4. Solenoid valve output interface
- Connection to the argon gas connector of the welding gun. 5. Negative Quick connector
- Negative quick connector socket for connection to welding gun. 6. Parameter size adjustment knob
- When the function buttons select different functions, you can use this knob to adjust the parameter size/value. 7. Welding parameter selection button
- Through this button, you can select the front gas, hot arc starting, arc starting current, slow rise, welding current, slow drop, end arc current, rear gas and other functions. 8. AC parameter selection button
- Through this button, you can select AC frequency, duty cycle, pulse width cleaning and other functions. 9. Welding mode selection button
- This button can be used to select manual welding, DC argon arc welding, pulse argon arc welding and other functions. 10.AC/DC selection button
- Use this button to select DC or AC mode. 11.Welding waveform selection button
- Through this button, you can select four output waveform processes: square wave, triangle wave, trapezoidal wave, and sine wave according to the technological effect that the welding workpiece needs to achieve. 12.Channel and save selection button
- Through this button, the set parameters can be stored, which is convenient for direct call-up for the next task. This function can save ten parameter settings with codes 0-9.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com 13.2T/4T selection button
- The 2T/4T function can be selected through this button. 14.Repeat/spot welding selection button
- Use this button to select the repeat and spot welding functions according to the workpiece material and process requirements. 15.Pulse parameter selection button
- Use this button to adjust the peak current, base current, duty cycle and other parameters. 16.Welding parameter selection button
- With this button you can select the front gas, hot arc starting, arc starting current, slow rise, welding current, slow drop, end arc current, rear gas and other functions. 17.Solenoid valve input interface
- Connection with argon gas cylinder. 18.Power cable entry 19.On/Off power switch LOOSE ITEMS SUPPLIED INCLUDE THE FOLLOWING:
- 1 x TIG Torch /Cable assembly.
- 1 x Earth Cable/Clamp
- 1 x Gas Hose
- 2 x hose clamps
- 3 x Gas shrouds (5, 6 & 7mm)
- 4 x Tungsten collars (1.6, 2, 2.2 & 2.4mm)
- 1 x Tungsten electrode
- 1 x Long torch end cap
- 1 x Short torch end cap
- MMA welding lead
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com PREPARING THE WELDER FOR USE To prepare the machine for welding it is important that you follow the following procedure. Making sure that the ON/OFF switch, located on the rear panel is in the OFF position. Connect the welding leads and gas bottle as follows and set the selector switch to the position shown. The welder can be configured to weld, with or without a gas supply according to the type of welding wire being used.
- Mild steel solid core (with gas)
- Flux cored (no gas) Connect a bottled gas cylinder to the connector at the back of the welder. Switch on using the switch located on the rear panel. Attach the earth clamp to the workpiece as close as possible to the area being welded. Clean with a wire brush where necessary to ensure the connection is as clean as possible.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com PREPARING THE TIG TORCH Alternative torch components are supplied with the unit and are assembled is as follows. 1. Unscrew and remove the end cap (E). 2. Select the size of electrode required, and ensure you select the correct size collet body for that particular electrode. 3. Screw the collet body (A) into the head of the torch and tighten finger tight and then screw on the gas shroud (B). 4. Thread the electrode (D) through the collet (C), and insert the collet into the collet body (A) through the rear of the head with its shoulder facing the rear as shown. 5. Push the electrode in, so that it protrudes from the nozzle by approx. 10mm and screw on the long end cap (E). As the end cap tightens, the electrode will be gripped and secured in position. 6. Whilst it is still possible for the electrode to move, adjust it so that it protrudes from the nozzle by 4 - 5mm, and then tighten the end cap against the rubber O-Ring. The electrode should be approx the same thickness as the workpieces being welded.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com NOTE: Before assembly, file or grind the tip of the electrode to a point (from 40-60 deg) as this will give optimum performance. The following electrode sizes can be used and are available from your CLARKE dealer. PREPARING THE WORKPIECE The area being welded should be perfectly clean. Any coating, plating or corrosion must be removed, otherwise a good weld will be impossible to achieve. ATTACHING THE EARTH CLAMP Attach the earth clamp firmly to the workpiece as close as possible to the point of weld. IMPORTANT: Ensure that the earth clamp is attached to clean, solid metal necessary, thoroughly clean with a wire brush or similar to guarantee a good connection. ELECTRODE DIAMETER WORKPIECE THICKNESS MMA 1.6 mm 1.5 - 2.0 mm 2.5 mm 2.5 - 3.0 mm 3.2 mm 3.5 - 4.5 mm TIG 1.2mm Tungsten 1.0 - 2.0mm 2.4mm Tungsten 2.5 - 3.0mm
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com CONTROL SETTINGS DISPLAYED Refer to page 14 for basic control panel functions UPPER SCREEN 1. Set the AC/DC setting as required.
- AC is for aluminium.
- DC is for carbon steel/stainless steel. 2. This selects the welding method;- either
- MMA,
- HF-TIG (pure argon), or
- HF TIG pulse (pure argon). 3. When you start welding, the arc can have a different shape.
- Press the selection button to choose one. 4. This control is used to save a group of parameters ready for when you return to welding next time.
- PROG
- SAVE
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com 5. When selecting 4T, there is no need to hold the trigger continuously during welding. 6. If selecting Repeat, the machine repeats the output between the two currents set, from strong to weak and from weak to strong. Spot welding should be easy to use. LOWER SCREEN 7. This display range is for AC welding. Displayed is the AC pulse frequency and the lower LEDs show;
- IH - Hot starting current
- Ii - striking current
- Tup - upslope time
- I - welding output current
- Tc - clean time
- clean - clean width.
- the Gas Bottle means Pre-gas time setting
- AC/HZ - AC frequency 8. This display belongs to the Pulse range. Turn to the TIG Pulse channel to enable settings in this range and the lower LEDs show;
- IP - Pulse peak current setting
- IB - Pulse base current setting
- T-DOWN - downslope time
- I-2 - crater arc current
- symbol - pulse duty ratio
- the Gas Bottle means post-gas time setting
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com OPERATING THE WELDER (MMA) The consumable electrode is connected to a high amperage low voltage supply which creates an electric arc between the electrode and the workpiece. The most difficult aspect of the arc welding process, particularly for beginners, is that of striking an arc. We strongly recommend that you practice on some pieces of scrap metal to get the feel of the operation before you start an actual welding job. 1. Holding the welding mask close-up to your face, give a short stroke with the electrode on the workpiece. As soon as the arc is primed, withdraw the electrode from the workpiece to leave a gap. The current will flow across the gap with a crackling noise and a brilliant arc. Continue to weld in one direction, maintaining the small gap as you go. 2. As soon as the arc is struck, maintain a distance from the workpiece equal to the diameter of the electrode. Keep this distance as constant as possible for the duration of the weld. As you advance along the workpiece the angle of the electrode must be maintained at between 20º and 30º. NOTE: When you prime the arc be sure to withdraw the electrode swiftly to leave the gap, otherwise the electrode will weld itself to the workpiece. If this occurs give the electrode a short sharp jerk to free it and, if necessary, prime the arc again. If you cannot free the electrode, switch the machine off immediately and free it. Take care the electrode will get red hot very quickly and will be capable of burning through welding gloves. 3. At the finish of the weld, bring the end of the electrode backward in order to fill the weld crater and then quickly lift the electrode from the weld pool to extinguish the arc. 4. Inspect the job carefully. Any slag forming on the surface should be chipped away with a chipping hammer or pick. ALWAYS wear your safety goggles when chipping away slag. WARNING: WHEN WELDING ALWAYS ENSURE THERE IS ADEQUATE VENTILATION IN THE WORK AREA DUE TO TOXIC FUMES. WARNING: DO NOT STRIKE THE ELECTRODE ON THE WORKPIECE, AS THIS MAY DAMAGE THE ELECTRODE. WARNING: WELDING ARCS PRODUCE HARMFUL UV/IR LIGHT WHICH CAN SERIOUSLY DAMAGE YOUR EYES. ALWAYS USE A WELDING FACE-SHIELD WITH A SUITABLE FILTER THAT CONFORMS TO CURRENT STANDARDS. WARNING: PROTECT BYSTANDERS BY USING WELDING SCREENS.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com OPERATING THE WELDER (TIG WELDING) TIG welding is primarily for very thin materials using a non-consumable tungsten (or tungsten alloy) electrode held in the torch. A shielding gas (100% Argon), is fed through the torch to protect:
- The electrode
- Molten weld pool
- Solidifying weld metal from contamination by the atmosphere The electric arc is produced by the passage of current through the conductive, ionized shielding gas. The arc is established between the tip of the electrode and the work. Heat generated by the arc melts the base metal. Once the arc and weld pool are established, the torch is moved along the joint and the arc progressively melts the joined surfaces. Filler wire, if used, is usually added to the leading edge of the weld pool to fill the joint. This process is ideally suited for welding thin metals such as car body panels, pressure vessels, heat exchangers, pipes etc., where accuracy and a high quality weld is desired, as it produces a very low porosity weld. MAIN FEATURES OF TIG WELDING 1. Electronic control of welding current. 2. Forced air cooling. 3. A thermal overload protection device prevents overheating. TIG WELDING PROCESS ADVANTAGES
- It produces superior quality welds, generally free of defects.
- It is free of the spatter which occurs with other arc welding processes.
- It can be used with or without filler metal as required.
- It allows excellent control of root pass weld penetration.
- It can produce welds at high speeds.
- It allows precise control of the welding variables.
- It is capable of welding very thin material (0.5mm), without undue distortion. LIMITATIONS 1. Greater weld dexterity is required. 2. The DC output is not suitable for welding aluminium.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com TIG WELDING Before TIG welding, you must obtain the correct torch and a gas cylinder of 100% pure Argon. To prepare the machine for TIG welding, adopt the following procedure. 1. Plug the work clamp lead in to the +ve terminal and connect the work clamp to the workpiece.
- For good contact, the work clamp must be attached to clean bare metal. Clean with a wire brush where necessary. 2. Plug the torch lead to the -ve terminal. 3. Screw the pressure regulator on to the gas bottle tightly, and attach the gas hose to the inlet connector securely, with a hose clip. 4. Turn the pressure regulator knob to set a pressure of approx. 2.5kg/cm2 (35 lbf/ in2). 5. Ensure the electrode at the torch nozzle, protrudes by 4 - 5mm, also ensure that the electrode is sharply pointed with an angle of 40o- 60o if it is not, grind it to shape. 6. Set the machine in accordance with the thickness of the material to be welded and the size of tungsten electrode to be used. 7. Switch on using the switch mounted on the rear panel. 8. If the machine stops at any time and the buzzer sounds, the thermal overload may have intervened. Wait until the welder has cooled sufficiently before restarting work. 9. Cover your face with the head shield, bring the torch to within 3-4mm of the work, and at an angle of 40-60o, so that the ceramic nozzle gently touches the work surface. 10. Scratch the tip of the electrode against the piece to be welded, as soon as the welding arc starts, remove the electrode to a distance of 3-4 mm, and continue the weld. (See notes below).
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com
- This method is referred to as ‘Scratch Arc’. 11. To stop welding, simply remove the torch from the workpiece. 12. Turn off the gas as soon as you finish welding. Notes:
- To avoid a visible strike mark on the surface of the workpiece it is advisable to strike the arc in the joint where the mark will be concealed by the weld.
- Thin sheet and stainless steel may be welded with or without filler, similar to gas welding.
- The filler is fed in at the edge of the pool. The rod must not touch the tip of the electrode or enter the arc. The end of the rod must always be shielded by the argon atmosphere to prevent as far as possible the formation of oxides of its surface. When welding stainless steel and copper, it is often possible to feed in the filler continuously at the edge of the pool.
- The arc length generally varies between 3 and 6 mm depending on the type of joint, type and thickness of material and so on.
- The torch is advanced in the direction of welding, without lateral movement, maintaining the torch angle of 45o to the workpiece. NOTE: TIG DC welding is used for welding Aluminium and also for welding very thin material (0.5mm - 4mm max). It is very important, particularly when DC welding, to ensure that the workpiece is perfectly clean immediately before proceeding to weld. Remember that oxidation takes place very quickly with some materials, presenting a barrier which should be avoided if a high quality weld is required.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com WELDING PITFALLS The MMA and TIG welding technique is an acquired skill and requires considerable practice before perfect results are obtained. The diagrams below will help to explain the pitfalls in your technique and how to overcome them. ARC TOO SHORT This causes irregular masses of weld to be deposited, with slag contamination on an uneven surface. ARC TOO LONG This causes poor penetration resulting in a weak weld with excessive spatter and porosity. Surface of the weld is rough and the arc makes a hissing sound ELECTRODE MOVED TOO SLOWLY This causes a very wide and heavy deposit which overlaps at the sides. It is wasteful both in terms of time and electrode use. ELECTRODE MOVED TOO QUICKLY This causes poor penetration with a ‘stringy’ and incomplete weld deposit. Slag is very hard to remove. CURRENT TOO LOW This causes poor penetration and causes the electrode to stick to the workpiece too readily. Also results in a very irregular and high weld deposit. Slag is very hard to remove. CURRENT TOO HIGH This causes excessive penetration with spatter and deep pointed crater. It may also cause holes to be burned in the workpiece. Burns electrodes very quickly. THE PERFECT WELD With the correct combination of arc length, current regulation, inclination and speed of the electrode, you will, with practice, produce the perfect weld. This should be regular with uniform ripples and no slag contamination. The arc will make a steady crackling sound.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com TROUBLESHOOTING Your CLARKE Welder has been designed to give long and trouble free service. If however, having followed the instructions in this booklet carefully you still encounter problems, the following points should help identify and resolve them. DEFECT CAUSES SUGGESTIONS Spark will not start Bad clamp connection. Inverter printed circuit is defective. Check clamp connection. Contact your nearest CLARKE dealer. No output voltage Overheated machine (the amber LED should be on). Wait for thermal cutout to be reset. Internal relay has failed. Contact your nearest CLARKE dealer. Inverter printed circuit is defective. Contact your nearest CLARKE dealer. Wrong output current Current selector control is defective. Contact your nearest CLARKE dealer. Low power supply voltage. Check the mains distribution system. Porosity of welds Acid electrode on steel with high sulphur content. Electrode oscillates too much. Workpieces are too far apart. Workpiece being welded is cold. Use basic electrode. Move edges to be welded closer together. Move slowly at the beginning. Cracks in weld Material being welded is dirty (e.g.oil, paint, rust, oxides). Not enough current. Clean workpiece before welding is an essential method of achieving neat weld beads. Also increase current output. Limited penetration Low current, high welding rate, reversed polarity. Electrode inclined in position opposite to it's movement. Ensure operating parameters are regulated and improve preparation of work pieces. Profile defects Welding parameters are incorrect. Pass rate is not related to operating parameter requirements. Electrode not inclined constantly while welding. Follow basic and general welding principles.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com High Sprays Electrode is too inclined. Make appropriate corrections. Arc is unstable Insufficient current. Check condition of electrode and earth wire connection. Electrode melts obliquely Electrode core is not centred. Magnetic blow phenomenon. Replace electrode. Connect two earth wires to opposite sites of the work piece. No response from welder. Check fuses and power cable. Replace fuses as necessary. If problem persists return welder to your local dealer. Check fuse size. Poor quality welds. Insufficient gas at weld area. Check that gas is not being blown away by drafts and if so move to a more sheltered work area. If not, increase gas supply. Rusty, painted, damp, oil or greasy workpiece. Ensure workpiece is clean and dry. Rusty/dirty wire. Ensure wire is clean and dry. Poor earth contact. Check earth clamp/workpiece connection. Welder cuts out whilst in use. Duty cycle exceeded (auto cut- out operates). Allow welder to cool 15-30 mins before continuing. Note: If duty cycle is continually exceeded, damage to the welder may result and welder output is probably too small for application. Buzzer sounds Machine has overheated Machine will return to normal after temperature drops. Thermal relay has failed Replace relay. Power supply voltage is too low Machine will operate after power supply is restored. No argon gas output No gas Solenoid valve broken Connecting tube blocked Check the flow meter and gas supply. Check pipeline is clear. DEFECT CAUSES SUGGESTIONS
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com CARE AND MAINTENANCE The machine requires no maintenance other than the following guidelines. Cleaning at frequent intervals is advisable if the unit is operating in a very dusty environment. Avoid getting particles of metal inside the machine since they could cause short circuits. 1. Keep the casing louvres clean to avoid a build up of dirt and oxides inside the machine which can reduce machine output. 2. Check all cables periodically for good condition and security. 3. Always inspect the earth cable and torch hose before use, to ensure they are in perfect condition and that the earth clamp is clean and secured correctly to the cable. 4. Check the hose for security and damage. Contact tip The contact tip is a consumable item and must be replaced when the bore becomes enlarged or oval. The contact tip MUST be kept free from spatter to ensure an unimpeded flow of gas. To keep the contact tip free from spatter, we recommend the use of anti-spatter spray (6000715) available from your CLARKE dealer. Torch shroud The torch shroud must also be kept clean and free from spatter. Build-up of spatter inside the gas cup can cause a short circuit at the contact tip which will result in expensive machine repairs. WARNING: ELECTRICITY CAN KILL - NEVER TOUCH LIVE ELECTRICAL COMPONENTS. WARNING: DISCONNECT THE POWER SUPPLY BEFORE ALL INSPECTION AND MAINTENANCE OPERATIONS. BEWARE HOT SURFACES.
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com COMPONENT PARTS
1 Potentiometer & knob 14 Rear panel 27 Output copper bar 2
2 Fix panel 15 Upper windshield? 28 Gun switch plate
3 Panel 16 Circuit breaker 29 Output copper bar
4 Front control PCB 17 Cable gland 30 Current transformer
5 Casing 18 Soft-start fan 31 Base plate
6 Lifting handle 19 Solenoid valve 32 Express socket
7 AC converter board 20 Radiator 1 33 Aviation socket
8 Middle separator 21 Rectifier bridge 34 Socket fixing plate
9 Radiator 3 22 Epoxy plate 1 35 Aviation socket
10 Main control board 23 Main circuit board 36 Gas connector
11 Epoxy board 24 Output copper bar 1 37 Front panel
12 Aluminium resistance 25 Circuit board prop
13 Absorber plate 26 Connecting copper bar
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com TORCH COMPONENT PARTS No Description No Description
1 End Cap c/w O-ring 6 Ceramic Nozzle
2 Front Cup Gasket 7 Tungsten Electrode 1.6/2.4 mm
3 Torch Body 8 Short end cap & O-ring
4 Collet 9 Hose & protective sleeve
5 Collet Sleeve
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com MACHINE RATING PLATE This welder is covered by regulations EN 60974-1:2018+A1:2019 / EN 60974- 10:2014+A1:2015, where the Duty Cycle is expressed as a percentage of time the machine may be used in a given period for a specified welding current. e.g. When welding at 140 Amps the machine may be used for 6 minutes (60%) in any10 minute period.
1 Name/address of manufacturer 9 Energy Supply symbol
2 Model Number 10 Electrode symbol
3 Part number 11 Rated No-load Voltage
4 Welding Power Source 12 Max Effective Supply Current
5 Standards applied 13 Insulation grade
6 Welding Process symbols 14 Rated Supply Voltage
7 Degree of Ingress Protection 15 Rated Maximum Supply Current
8 Min & max welding current and
corresponding load voltages
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com CONSUMABLES & ACCESSORIES The following are some of the accessories available from your CLARKE dealer. Please quote the part numbers shown below: A Gas Regulator, Arc Activated Headshields, Anti-spatter Spray, Swan Necks, Torch Shrouds and Torch Liner are also available from your CLARKE dealer or our parts division. Part Description Part number Comment Welding Gas CO2 (250g) 6000642 For welding mild steel CO2 (600g) 6000643 For welding mild steel Argon 6000661 For aluminium/stainless CO2/Argon Mix 6000660 For welding stainless/ thin sheet mild steel Arc Welding Rods 1.6 x 300mm 3050590 2.0 x 350mm 3050592 2.5 x 350mm 3050594 3.25 x 350mm 3050596 Welding Rods 4.0 x 400mm E6013 3050598 Welding Torch Welding Torch Assembly (MMA/TIG) 6012232 Regulator Argon Gas Regulator 8134140 Anti-splatter spray 500ml aerosol 6000715 Welding Apron 6000920 Gauntlets Leather (EN407 rated) 8133492 Welding screen WSC2 and replacement screen 6000945 6000910
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com ARC ACTIVATED HEADSHIELDS These highly popular head-shields activate instantly when the arc is struck and allow you to have both hands free when welding. GUARANTEE This CLARKE product is guaranteed against faulty manufacture for a period of 12 months from the date of purchase. Please keep your receipt as proof of purchase. This guarantee is invalid if the product is found to have been abused or tampered with in any way, or not used for the purpose for which it was intended. Faulty goods should be returned to their place of purchase, no product can be returned to us without prior permission. This guarantee does not effect your statutory rights. Model Arc Activated Grinding function Solar Powered Fixed Shade Flip Up Part Number GWH4 X X X 6000706 GWH5 X X X 6000707 GWH6 X X X 6000708 GWH7 X X X 6000709 GWH8 X X X 6000714 PG4 X X X 6000716 HS1 X X 6000700 HSF1 X X 6000705
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com DECLARATION OF CONFORMITY -UK
Parts & Service: 020 8988 7400 / E-mail: Parts@clarkeinternational.com or Service@clarkeinternational.com DECLARATION OF CONFORMITY - CE